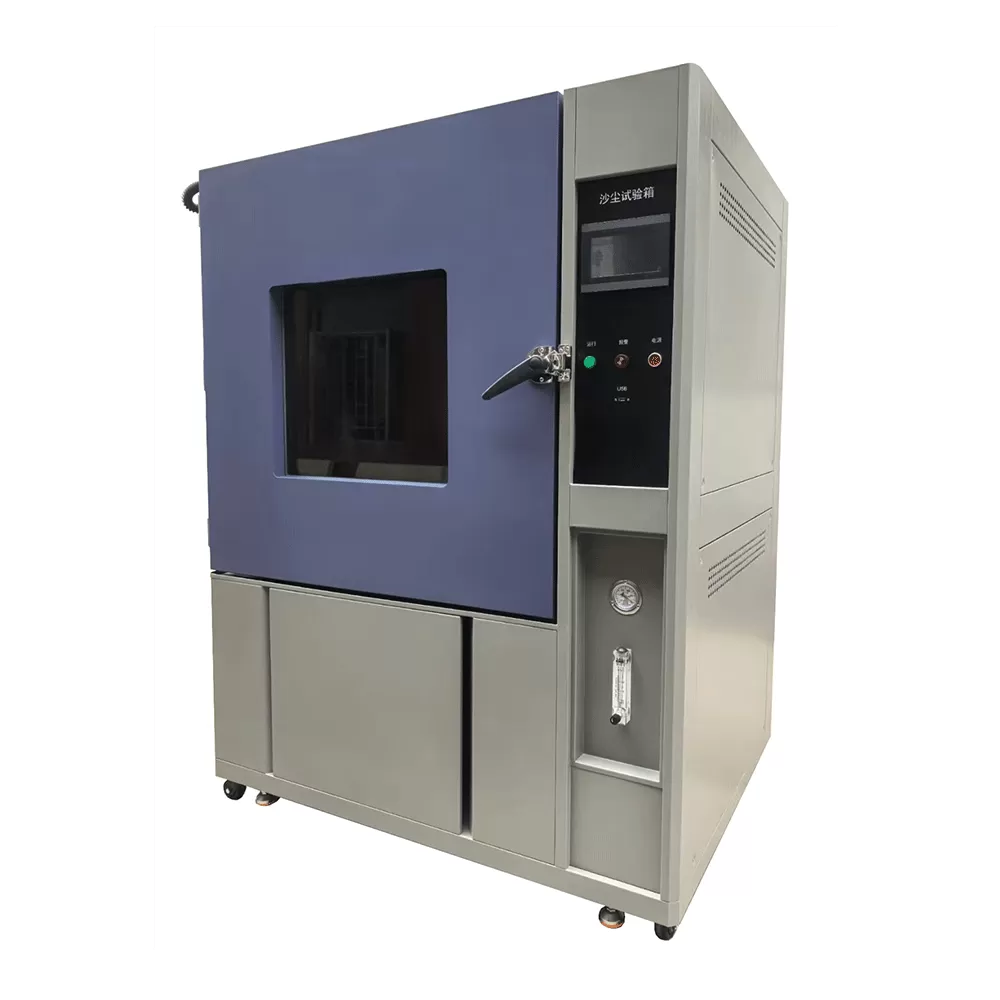
Particulate ingress remains one of the least forgiving failure modes in outdoor electronics, automotive lighting, connector assemblies, and photovoltaic hardware. A single grain of fine mineral dust reaching a bearing surface or a sealed contact can change electrical behavior and mechanical wear over a product's service life. Because field exposure takes years to produce measurable results, engineering teams reproduce the process in a dust chamber where concentration, airflow, humidity, and pressure differential can be held to defined values.
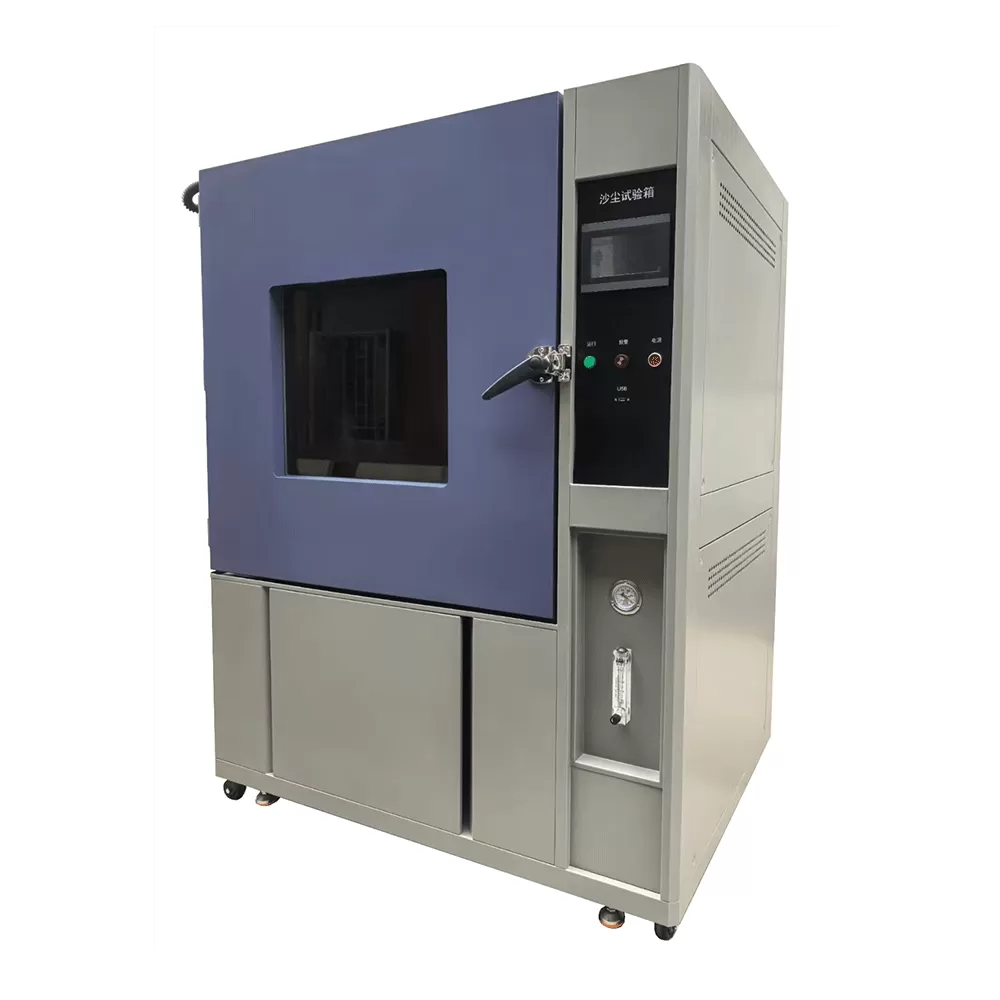
What a Dust Chamber Actually Reproduces
Dust ingress is not a single mechanism. Particles settle under gravity, travel on air currents, migrate through pressure-driven leaks, and accumulate around gaskets and cable entries. Thermal cycling opens and closes microscopic gaps, while vibration works abrasive material into seams. An effective test system therefore has to control several physical variables at once rather than simply filling a cabinet with powder.
Two operating modes dominate laboratory practice. Free-settling exposure suspends powder gently and allows it to descend onto the sample, which reflects installations such as roadside cabinets and rooftop enclosures. Circulating exposure keeps dust airborne with blowers or injection nozzles so the sample faces continuous particle impingement, reproducing vehicles, turbines, and equipment mounted near moving air. Some chambers support only one mode, while configurable platforms switch between them.
The particle specification matters as much as the mode. Fine talcum powder behaves very differently from coarse sand or from blended test dusts such as Arizona Test Dust, red kaolin, or silica flour. Particle size distribution, moisture content, and angularity all affect how material penetrates a gasket and how it settles inside the chamber. Treating every powder as interchangeable produces data that cannot be compared across laboratories or repeated across production batches.
Standards That Define Chamber Test Parameters
Test parameters come from product standards, not from chamber design preferences. The equipment must be able to hold whatever the referenced document demands, which is why specification review comes before dust chamber selection.
IEC 60529 and the IP5X / IP6X Enclosure Ratings
IEC 60529 remains the reference for ingress protection ratings worldwide. Clause 13.4 covers dust testing with talcum powder that passes a 75 µm sieve, with at least 50 percent of the mass passing a 45 µm sieve. The standard calls for a concentration of roughly 2 kg of powder per cubic meter of chamber volume and a test duration of 8 hours. For the IP6X rating, the sample is additionally evacuated so that the internal pressure stays below the surrounding pressure by no more than 2 kPa, with an air extraction rate between 40 and 60 times the sample volume per hour.
That vacuum requirement is where many facilities fall short. Without calibrated, independent extraction control per test item, the pressure differential drifts, and the resulting test does not represent the rating being claimed.
Automotive and Aerospace Requirements
ISO 20653 adapts the IP framework for road vehicles and defines dust classes that reflect under-hood and exterior mounting positions. MIL-STD-810 Method 510 covers blowing dust and settling dust procedures with defined dust concentration, wind velocity, and duration values, and is common for defense and ruggedized equipment. RTCA DO-160 Section 12 addresses airborne avionics, where fine dust combined with altitude-related pressure changes produces demanding conditions.
IEC 60068-2-68 Environmental Test L
This standard group separates test L into variants covering airborne dust and sand, free settling dust, and high-velocity sand-laden airflow. Chambers intended for these methods need adjustable airflow velocity and, in some configurations, temperature control to match the referenced profile.
Technical Anatomy of a Reliable Dust Chamber
Mechanical construction decides whether a chamber produces repeatable data or merely plausible-looking results. Four subsystems carry most of the responsibility.
Cabinet Geometry and Airflow Management
Internal volume has to be sized around the sample, its fixture, and the required clearance for airflow. Sharp corners and structural ledges create dead zones where powder accumulates instead of circulating. A well-designed chamber uses radiused internal surfaces, a dedicated return duct, and a diffuser that distributes air across the full working section. Computational fluid dynamics modeling during design confirms that velocity and concentration remain within tolerance across the usable volume rather than only near the injection point.
Stainless steel 304 or 316 interior for corrosion resistance and easy cleaning
Laminated or tempered viewing window with interior illumination
Glove ports or a rapid access hatch for in-test adjustments
Interlocked door and safety logic to prevent powder release during operation
Dust Feeding and Concentration Stability
Getting powder into the airstream at a constant rate is harder than it appears. Talcum powder cakes under humidity, bridges in hoppers, and clumps in feed lines. Venturi injectors, fluidized beds, and screw feeders each handle this differently. A gravimetric feeder with feedback from a downstream concentration sensor holds the setpoint far more reliably than a timed auger alone.
Heated or dehumidified supply air to prevent agglomeration
Continuous hopper agitation and level sensing for automatic refill
Secondary dispersion nozzle to break remaining clusters
Sample port for gravimetric or optical concentration verification
Pressure Differential and Vacuum Circuitry
Rating claims such as IP6X depend on a controlled vacuum inside the test item. Each sample position needs its own adjustable valve, flow meter, and pressure transducer so that one item's leakage does not affect another. Data logging of differential pressure and extraction flow across the full test duration turns a pass or fail statement into an auditable record.
Control, Instrumentation, and Data Integrity
Modern controllers store test recipes, enforce calibration intervals, and export time-stamped records. For regulated industries, the value lies in traceability: which powder batch was used, what the measured concentration was, how long the sample was exposed, and whether any deviation occurred. A chamber that cannot produce that record creates rework during audits.
Selection Criteria and Operational Challenges
Most procurement mistakes trace back to mismatched expectations between the test standard and the equipment specification. The following points surface repeatedly during dust chamber specification reviews.
Volume versus throughput: oversized chambers dilute concentration control and waste powder, while undersized units limit sample size and throughput.
Concentration uniformity: verify with mapping data, not with a single-point reading taken near the injector.
Powder recovery and cleaning: residue left from a previous test contaminates the next one and skews results.
Operator exposure: respirable mineral dust requires sealed operation, filtered exhaust, and documented safe-change procedures.
Filter loading: bag and HEPA stages need differential pressure monitoring so maintenance is scheduled before airflow drops.
Vacuum accuracy: low-range differential sensors and calibrated needle valves determine whether IP6X testing is defensible.
Powder traceability: batch certificates for particle size distribution and moisture support long-term comparability.
Addressing these points during design costs far less than retrofitting a chamber after a failed audit or an inconsistent round-robin comparison with an external laboratory.
Maintenance, Verification, and Lifecycle Planning
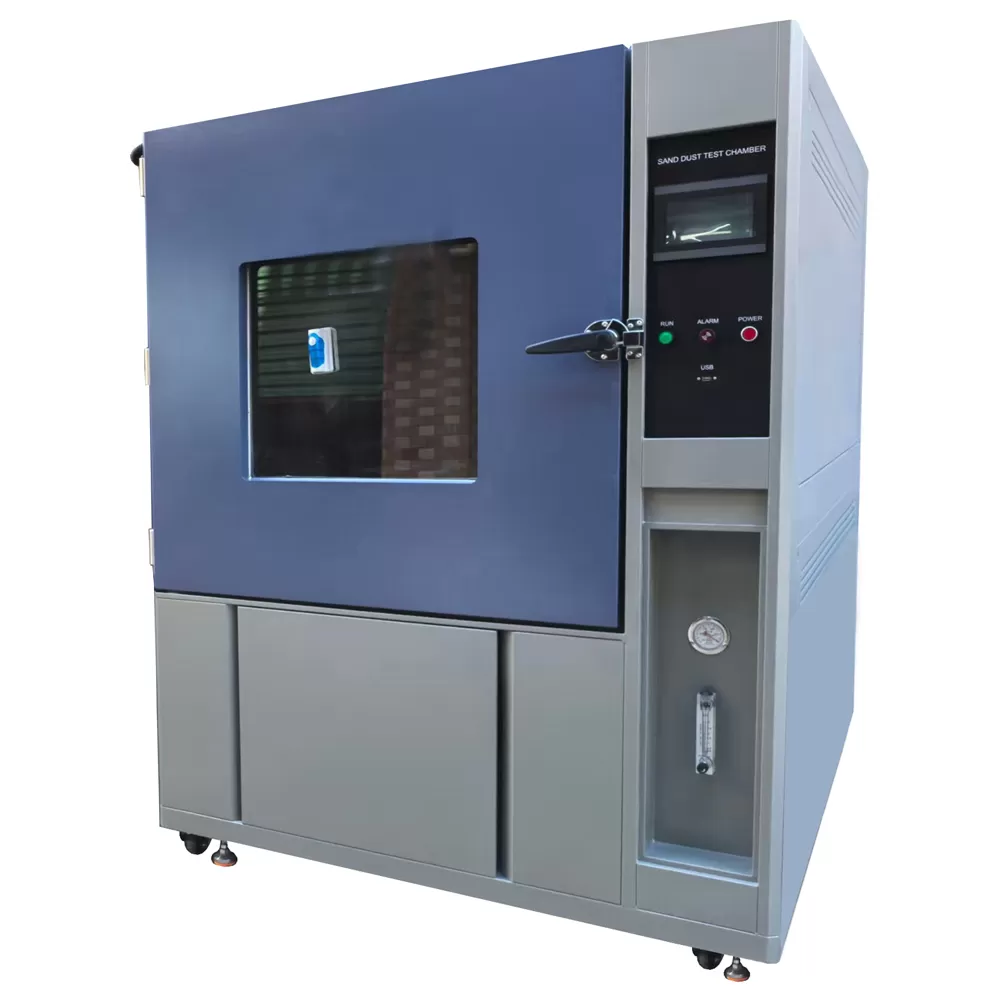
Performance drifts as filters load, seals age, and powder residue accumulates on duct surfaces. A practical maintenance regime includes scheduled interior cleaning, filter replacement based on differential pressure rather than calendar intervals, verification of airflow velocity at defined grid points, and annual concentration mapping. Pressure and flow instruments should be calibrated against traceable references on a defined cycle, with certificates retained alongside test records.
Consumables planning deserves attention as well. Powder lots vary, and switching suppliers mid-programme can shift results enough to require re-baselining. Keeping a documented powder specification and a retained sample from each lot supports comparability across years of testing.
HAOEN designs and builds environmental simulation equipment for laboratories that need documented, repeatable results, and the engineering team supports specification review, chamber sizing, and integration with existing test benches. Whether the target is a single IP6X qualification or a multi-standard programme spanning automotive, aerospace, and consumer electronics, matching the dust chamber to the referenced method is what makes the data defensible.
Frequently Asked Questions
What is the difference between IP5X and IP6X dust testing?
Both ratings use the same talcum powder and the same 8-hour exposure in most product standards. IP6X adds active evacuation of the test item, which pulls airborne particles into the enclosure through any leak path. IP5X relies on settling and light circulation without a pressure differential, so a product can pass IP5X and still fail IP6X.
How long does a typical test run?
IEC 60529 specifies 8 hours for dust testing. Automotive, military, and aerospace standards define their own durations, sometimes with repeated cycles or combined temperature profiles. Chamber design should support the longest profile in the facility's scope of work without exceeding concentration tolerances.
Which dust type should be used?
Use the powder named in the referenced standard. IEC 60529 requires fine talcum powder with a defined sieve profile, MIL-STD-810 references Arizona Test Dust, and several aerospace documents specify silica-based blends. Substituting materials invalidates the comparison even when the visual result looks similar.
Can one chamber handle both free-settling and circulating dust modes?
Yes, if the airflow system includes variable-speed circulation, a settling mode with reduced turbulence, and switchable injection. The trade-off is control complexity and cost. Facilities that test to a single method often choose a dedicated configuration instead.
How is dust concentration verified inside the chamber?
Gravimetric sampling remains the reference method: a known volume of chamber air is drawn through a pre-weighed filter, and the collected mass determines concentration. Optical sensors can provide continuous trend data, but they should be correlated against gravimetric results during commissioning and periodic verification.
What chamber volume is needed for a given sample?
A common starting point is a chamber volume at least ten times the sample envelope, though standards may impose their own ratios and clearance rules. Larger samples with complex geometry need more working space to avoid airflow shadowing and to keep concentration uniform around the item.
How often should the chamber be recalibrated?
Most quality systems require annual calibration of pressure, flow, temperature, and concentration instrumentation, with verification after any major repair or relocation. Facilities operating under accreditation schemes typically follow a shorter interval for vacuum control channels used in IP6X testing.
For laboratories evaluating a new dust chamber or upgrading an existing installation, sharing sample dimensions, target standards, and expected throughput allows the HAOEN engineering team to propose a configuration with verified concentration uniformity, calibrated vacuum control, and documented test records. Submit your test requirements, drawings, and qualification scope to request a detailed proposal.